response@rebellconveyors.com Plot L-42, M.I.D.C. Kupwad, Sangli 416436 +91 92258 18171
Home
Works
Applications
Why Rebell
Quality
Clients
Contact
Request a quote
  1. Home
  2. Catalogue
  3. Bulk Material Handling Systems
  4. Bucket Elevators

Bucket Elevators

High-Performance Bucket Elevators for Efficient Vertical Conveying

Bucket elevator manufactured by Rebell Engineers Pvt. Ltd. 5 – 100 TPH

At REBELL ENGINEERS PVT. LTD., we design and manufacture precision-engineered Bucket Elevators that offer reliable, efficient, and continuous vertical conveying of bulk materials. With years of experience and strong engineering expertise, we are a trusted Manufacturer, Supplier, and Exporter of Bucket Elevators serving a wide range of industries across India and abroad.

Our manufacturing facility is located in Sangli, Maharashtra, India, equipped with advanced fabrication and testing capabilities to ensure quality and performance in every unit.

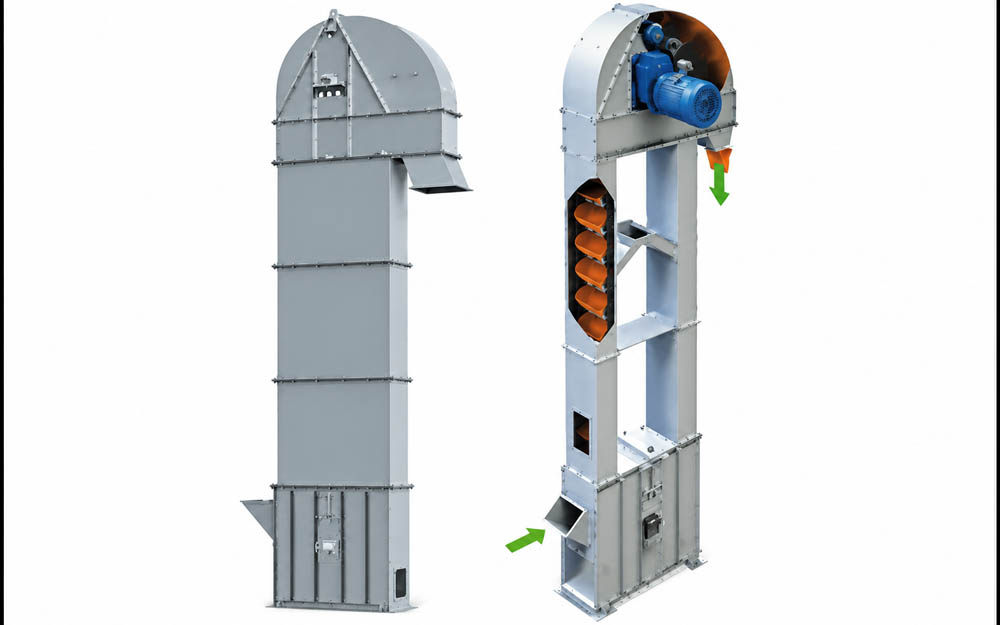
Bucket Elevators are specially designed systems used for vertical lifting and transportation of bulk materials from one level to another. These systems consist of a series of buckets attached to a belt or chain that rotates around two pulleys — one at the top and one at the bottom — efficiently carrying materials upward.

At REBELL ENGINEERS PVT. LTD., we manufacture both Belt Type (Twin Leg) and Chain Type (Self-Supported) Bucket Elevators, suitable for a variety of materials such as:

Whether handling free-flowing grains or abrasive industrial materials, our elevators are engineered for smooth operation, low power consumption, and high durability.

Key features

  • Custom-Built Designs: Tailored according to plant layout and material type.
  • Efficient Performance: Low power requirement with consistent material flow.
  • Compact Construction: Modular design saves installation space.
  • Smooth Operation: Reduced noise, vibration, and wear.
  • Durability: Fabricated using high-quality steel with corrosion-resistant coatings.
  • Ease of Maintenance: Quick access for inspection and service.
  • Reliable Output: Consistent throughput even under continuous operation.
Bucket Elevators

5 – 100 TPH

Request a quote
— Working principle

Bucket Elevators operate on a simple yet effective principle — a continuous chain or belt fitted with buckets rotates around two pulleys, lifting materials vertically.

— Technical specifications
Published data. Detailed sizing is confirmed against the duty.
TypeBelt Type (Twin Leg) / Chain Type (Self-Supported)
Capacity5 Ton/hour to 100 Ton/hour
Material of ConstructionMild Steel (MS) / Stainless Steel (SS) / Customized
Discharge TypeCentrifugal / Continuous
Drive MechanismDirect / Chain Drive
DesignModular, Compact, and Energy Efficient
OperationSmooth, Low Noise, Continuous
Capacity range5 – 100 TPH
TypesBelt type (twin leg), chain type (self supported)
Material handledFertiliser, loose sugar, grain, foundry sand, coal, bagasse
01

Belt Type Bucket Elevators (Twin Leg Design)

Our Belt Type Bucket Elevators are designed for high-speed, continuous vertical conveying of light to moderately heavy materials. These elevators feature a modular and compact design, allowing easy installation and maintenance even in restricted spaces.

  • Twin Leg, modular construction for stability and flexibility
  • Smooth and quiet operation with minimal vibration
  • Low power consumption and energy-efficient design
  • Dust-free operation with sealed enclosures
  • Suitable for fertilizers, sugar, grains, and other non-abrasive materials
  • Compact design saves floor space
02

Chain Type Bucket Elevators (Self-Supported Design)

Our Chain Type Bucket Elevators are designed for handling heavy, abrasive, and high-temperature materials. The chain mechanism provides superior strength and reliability for industrial-grade material handling requirements.

  • Robust self-supported structure for heavy-duty operation
  • Long-lasting chains with high tensile strength
  • Capable of lifting coarse, abrasive, and hot materials
  • Easy maintenance with accessible inspection doors
  • Designed for continuous duty under harsh conditions
  • Foundry sand, coal, clinker, and minerals

Applications

  • Sugar Industry: Conveying loose sugar and bagasse
  • Fertilizer Plants: Lifting granular and powdered fertilizers
  • Cement Plants: Vertical lifting of raw material and clinker
  • Food & Grain Processing: Handling cereals, grains, and pulses
  • Foundries: Transporting sand and similar materials
  • Power Plants: Handling coal and ash
  • Whether it's a process plant or a packaging unit, our elevators are engineered for dependable performance across applications.

Sectors served

— In detail

Materials handled

  • Fertilizer
  • Loose Sugar
  • Grain
  • Foundry Sand
  • Coal
  • Bagasse

Sequence of operation

  • Loading Section: Material enters the buckets from a hopper or conveyor at the base.
  • Lifting Section: The loaded buckets travel upward through a closed casing.
  • Discharge Section: Material is discharged at the top via centrifugal or continuous action.
  • Return Section: Empty buckets travel back down for refilling.
  • This mechanism ensures smooth, continuous, and dust-free conveying with minimal spillage.

Why Choose REBELL ENGINEERS PVT. LTD.?

  • Decades of Expertise: Trusted by major industrial sectors across India.
  • Quality Manufacturing: Designed and built under strict quality control at our Sangli facility.
  • Customized Solutions: Engineered to suit your exact conveying requirement.
  • Energy-Efficient Designs: Optimized for low power usage and minimal wear.
  • End-to-End Support: From design and installation to after-sales service.
  • Proven Reliability: Thousands of successful installations and satisfied customers.

Integration with Material Handling Systems

  • Belt Conveyor Systems
  • Screw Conveyors
  • Return Bagasse Carriers
  • This integration helps achieve seamless material flow, reduced manual handling, and optimized plant productivity.
  • For more information, visit our Bulk Material Handling Systems page.

Quality Assurance

Each Bucket Elevator from REBELL ENGINEERS PVT. LTD. undergoes rigorous inspection and testing to ensure durability and flawless performance. Our design team follows global engineering standards for load, speed, and material selection, ensuring maximum safety and operational efficiency.

  • We are committed to delivering equipment that offers consistent performance, long service life, and minimal downtime.

Need this sized for your plant?

Send the material, the tonnage and the centre distance or lift. We will come back with the specification.

Send your requirement