- Home
- Catalogue
- Bulk Material Handling Systems
- En-Mass Conveyor Systems
En-Mass Conveyor Systems
Efficient & Dust-Free En-Mass Conveyor Systems by REBELL ENGINEERS PVT. LTD.
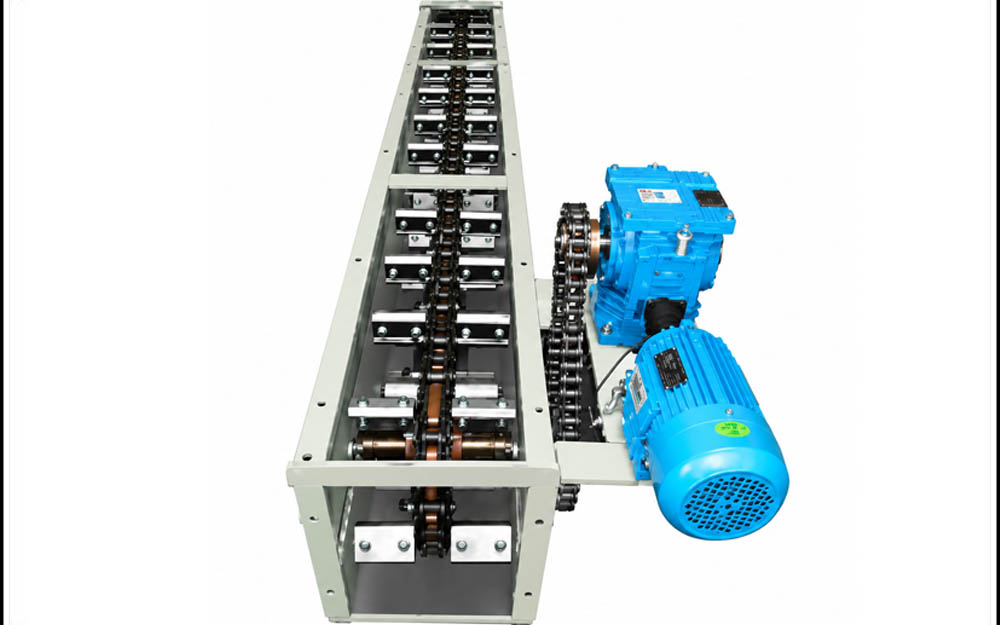 5 – 150 TPH
At REBELL ENGINEERS PVT. LTD., we specialize in the design and manufacturing of En-Mass Conveyor Systems that provide reliable, dust-free, and energy-efficient material handling solutions for a wide range of industries.
We are recognized as a trusted Manufacturer, Supplier, and Exporter of En-Mass Conveyor Systems, and our modern manufacturing facility is located in Sangli, Maharashtra, India.
Our En-Mass Conveyors are built to deliver high-capacity performance, low power consumption, and continuous conveying efficiency, making them an ideal choice for industries handling bulk materials like grain, rice, agro-vet raw materials, and fertilizers.
En-Mass Conveyor Systems are specialized chain-type conveyors designed for the horizontal or inclined transportation of bulk materials in a fully enclosed casing.
They operate on the principle of “en-masse movement,” where material moves in a solid, continuous column, propelled by flights attached to a moving chain. This results in a steady, controlled, and dust-free conveying process.
At REBELL ENGINEERS PVT. LTD., our En-Mass Conveyors are engineered to ensure minimum spillage, uniform flow, and long operational life, making them one of the most efficient conveying systems available.
Key features
- Efficient Conveying: Continuous, smooth material movement with minimal power use.
- Dust-Free Operation: Fully enclosed design ensures a clean working environment.
- Compact Construction: Saves space while maintaining high throughput.
- Low Maintenance: Few moving parts, easy access for inspection.
- Energy Saving: Reduced friction and low drive power requirements.
- Customizable Design: Adaptable to layout, capacity, and material type.
- Durable Build: Heavy-duty chain and flights designed for long life.
- Quiet & Reliable: Smooth and vibration-free operation for industrial environments.
| Capacity range | We manufacture En-Mass Conveyor Systems with a capacity range from 5 tons per hour to 150 tons per hour, depending on material characteristics and process requirements. |
|---|---|
| Conveyor Type | Horizontal / Inclined |
| Material of Construction | MS / SS / Custom Options |
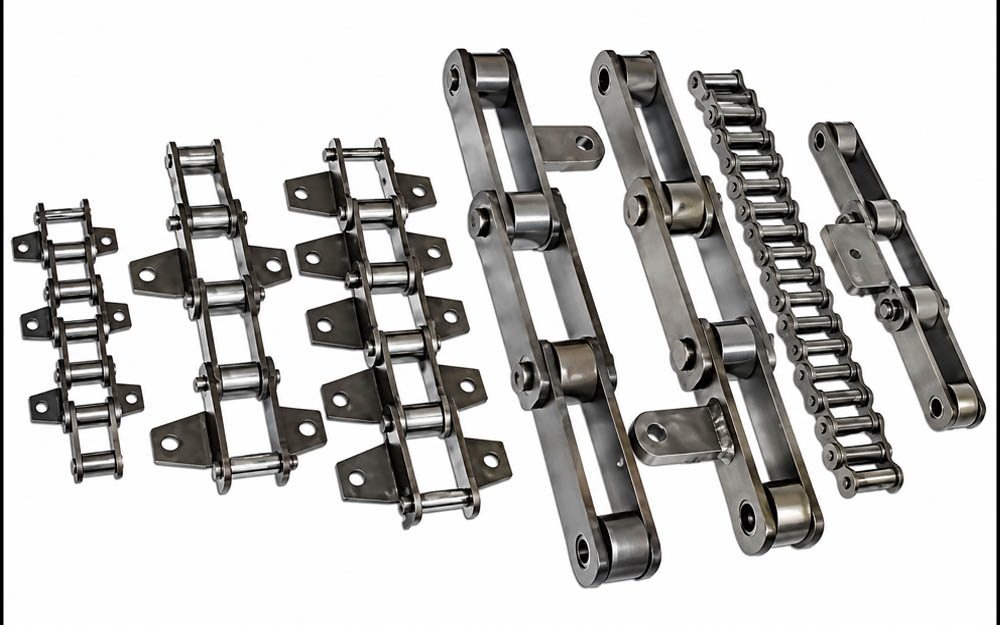
| Chain Type | Forged Steel / Drop-Forged / Roller Chain |
| Casing | Fully Enclosed Rectangular Design |
| Drive Type | Geared Motor / Chain Drive |
| Length | Up to 50 meters (Customizable) |
| Operation | Continuous & Dust-Free |
| Material handled | Grain, rice, agro-vet raw material, fertilisers |
Applications
- Our En-Mass Conveyor Systems are versatile and suitable for a wide range of materials and industries.
- Grain
- Ric
- Agro-vet Raw Material
- Fertilizers
- Cement
- Fly Ash
- Bagasse Dust
- Minerals and Powders
- Agro & Food Processing Units
- Fertilizer Plants
- Grain Storage & Rice Mills
- Chemical & Process Industries
- Sugar & Co-generation Plants
- Cement & Power Plants
- Their ability to convey different types of bulk solids efficiently makes En-Mass Conveyors a preferred choice for modern process industries.
Sectors served
Design & Construction
Every system is designed using advanced CAD software and manufactured under strict quality standards to ensure precision alignment, smooth operation, and minimal power loss.
- Our En-Mass Conveyor Systems are robustly designed, modular in construction, and precisely engineered for long-lasting reliability.
- Fully Enclosed Structure: Prevents dust generation and material spillage.
- Chain Mechanism: Uses forged or drop-forged steel chains with attached flights for strong and steady conveying.
- Drive Assembly: Geared motor or chain drive with variable speed control for flexible operation.
- Casing Construction: Built from high-quality mild steel (MS) or stainless steel (SS) for corrosion resistance and strength.
- Tensioning System: Spring or screw-based adjustment to maintain chain alignment.
- Inspection Openings: Provided for easy cleaning, maintenance, and inspection.
- Compact Layout: Suitable for restricted spaces and flexible installation.
How En-Mass Conveyor Systems Work
- The operation of an En-Mass Conveyor is based on a simple yet efficient principle:
- Material Loading: Bulk material enters through an inlet hopper.
- Chain Movement: A series of flights mounted on a chain drags the material forward.
- En-Masse Movement: The material moves in a solid bed (mass) within the casing.
- Discharge: The conveyed material exits through the discharge chute at the desired location.
- This enclosed, continuous flow mechanism ensures clean, safe, and efficient bulk material handling, even in dusty or demanding environments.
Advantages of REBELL En-Mass Conveyors
- Designed and manufactured in-house with precision engineering.
- Energy-efficient systems ensuring minimal operational costs.
- Proven performance across multiple process industries.
- Tailor-made designs for horizontal or inclined installations.
- Rugged construction for continuous, 24x7 operation.
- Easy integration with other bulk handling systems for complete automation.
- Long-term durability and service support from experienced professionals.
Integration with Bulk Material Handling Systems
- Belt Conveyor Systems
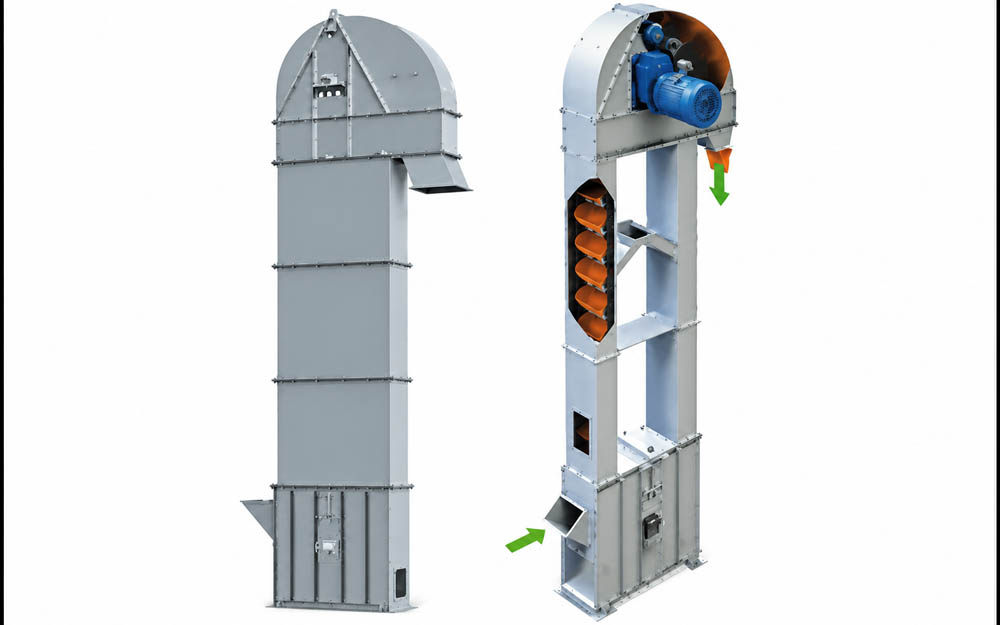
- Bucket Elevators
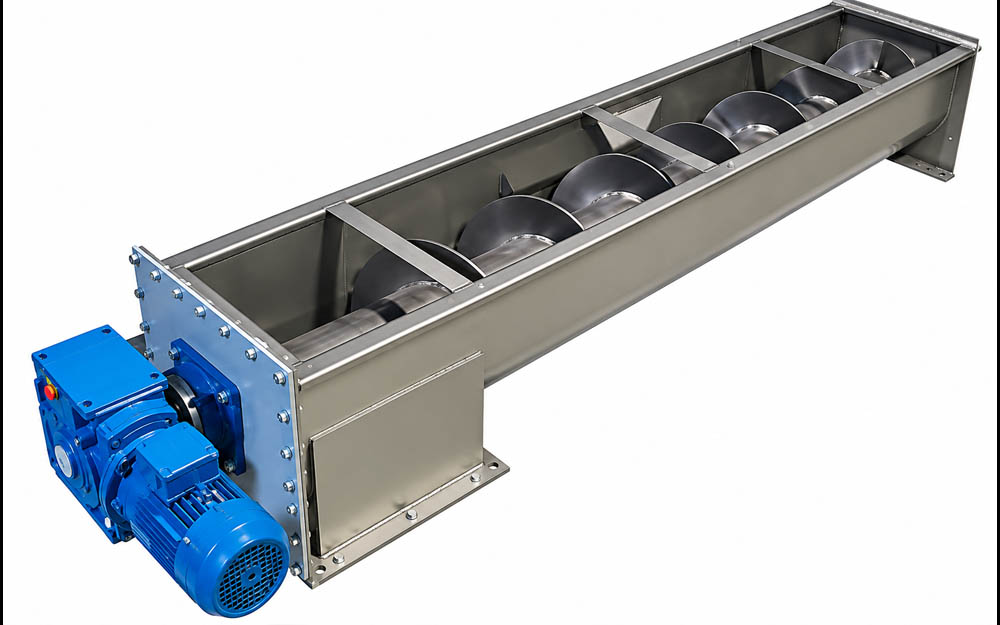
- Screw Conveyors
- Return Bagasse Carriers
- This integration ensures efficient plant operation, reduced downtime, and improved process flow across industries.
- ➡ Learn more about our Bulk Material Handling Systems.
Quality Assurance
At REBELL ENGINEERS PVT. LTD., quality and precision are at the core of our manufacturing philosophy.
- Accurate chain tension and alignment.
- High performance under load conditions.
- Compliance with industrial and ISO standards.
- Reliable operation and long service life.
- Proper material selection for corrosion and wear resistance.
- Our commitment to excellence ensures that every product delivers optimum efficiency, durability, and safety in every application.
Industries We Serve
- Our En-Mass Conveyor Systems are trusted by: ✅ Agro & Food Processing Plants ✅ Sugar & Co-generation Plants ✅ Fertilizer & Chemical Industries ✅ Cement & Power Plants ✅ Starch & Paper Industries ✅ Biomass & Renewable Energy Projects
Why Choose REBELL ENGINEERS PVT. LTD.?
- Decades of Expertise: Proven engineering experience in conveyor design and manufacturing.
- Custom Engineering: Solutions tailored to specific plant layouts and material needs.
- Complete In-House Production: Design, fabrication, assembly, and testing under one roof.
- Trusted by Industry Leaders: Installed in major plants across India and overseas.
- Prompt Service & Support: Dedicated technical team for maintenance and assistance.
- Commitment to Quality: Delivering reliable, high-performance systems consistently.
Need this sized for your plant?
Send the material, the tonnage and the centre distance or lift. We will come back with the specification.