Typical Rebell solutions
- Screw conveyors
- En-mass conveyors
- Heat exchangers
Rebell Engineers supplies material handling equipment and systems on a turnkey basis to the chemical sector. Send the material, tonnage and layout, and the system is specified to the duty.
Working in chemical?
Tell us the material and the throughput, and we will come back with what suits the plant.
Send requirement
02
Equipment for this sector
01
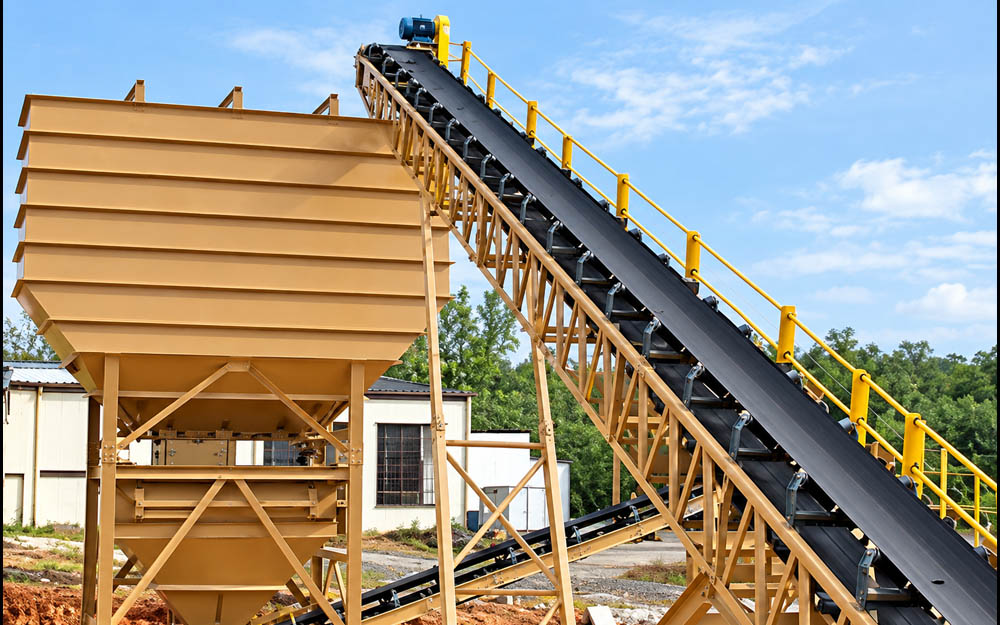
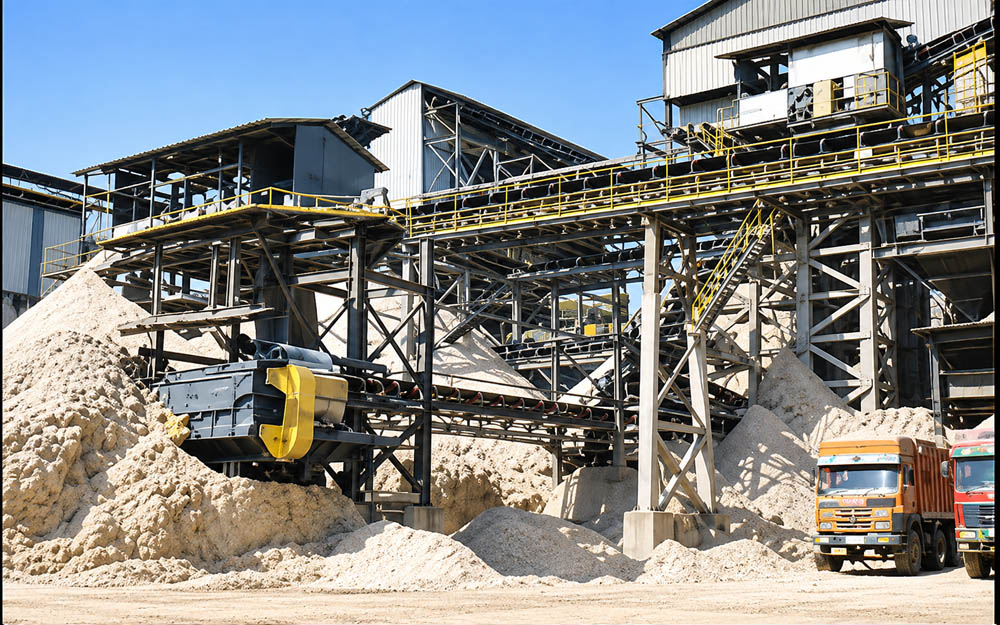
Belt Conveyor Systems
Trough and flat belt conveyors for bagasse, ash, coal, sand, salt and loose sugar, sized to the plant's throughput.
5 – 1000 TPH
02
Return Bagasse Carriers & Elevators
Carriers and elevators that return loose bagasse from the mill to the boiler, sized for continuous season-long running.
5 – 200 TPH
03
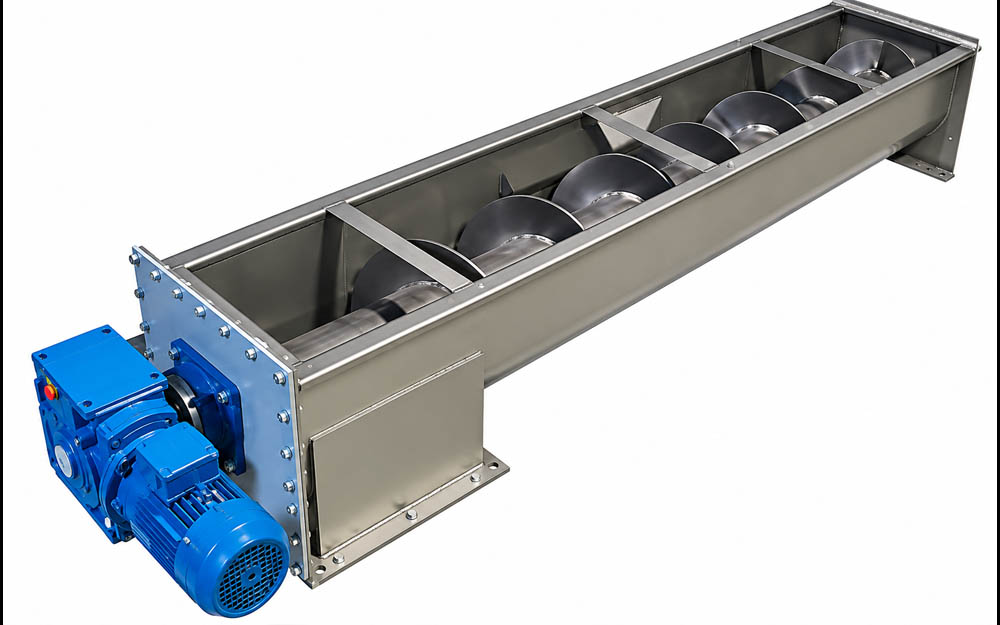
Screw Conveyors
Screw conveyors for sand, grain, sugar, fertiliser, seeds and ash — used across cattle feed, sugar, starch, chemical and fertiliser plants.
5 – 60 TPH
04
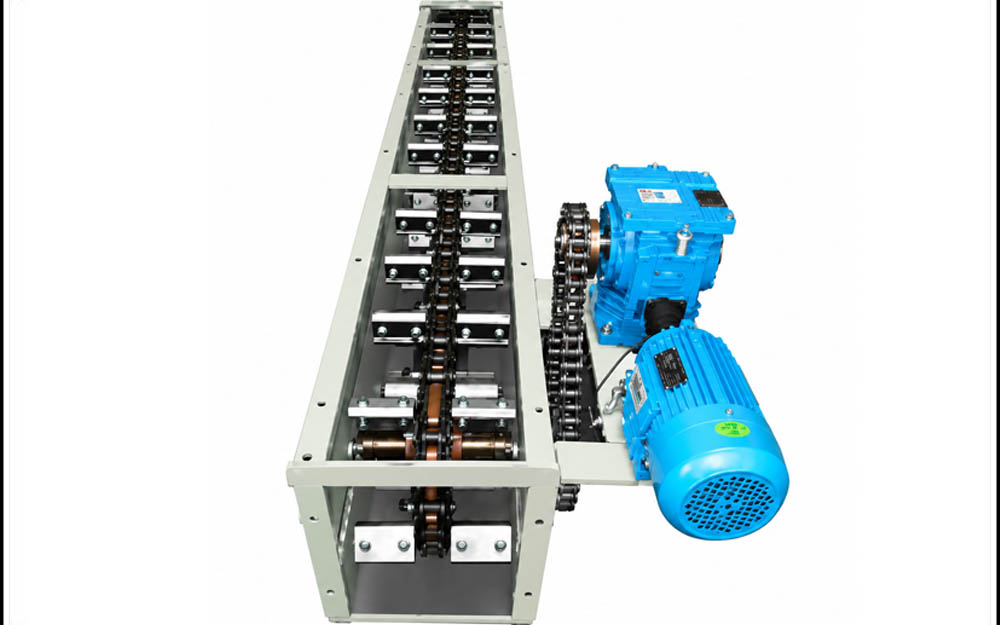
En-Mass Conveyor Systems
Enclosed en-mass conveyors for grain, rice, agro-vet raw material and fertilisers, with dust-free operation.
5 – 150 TPH
05
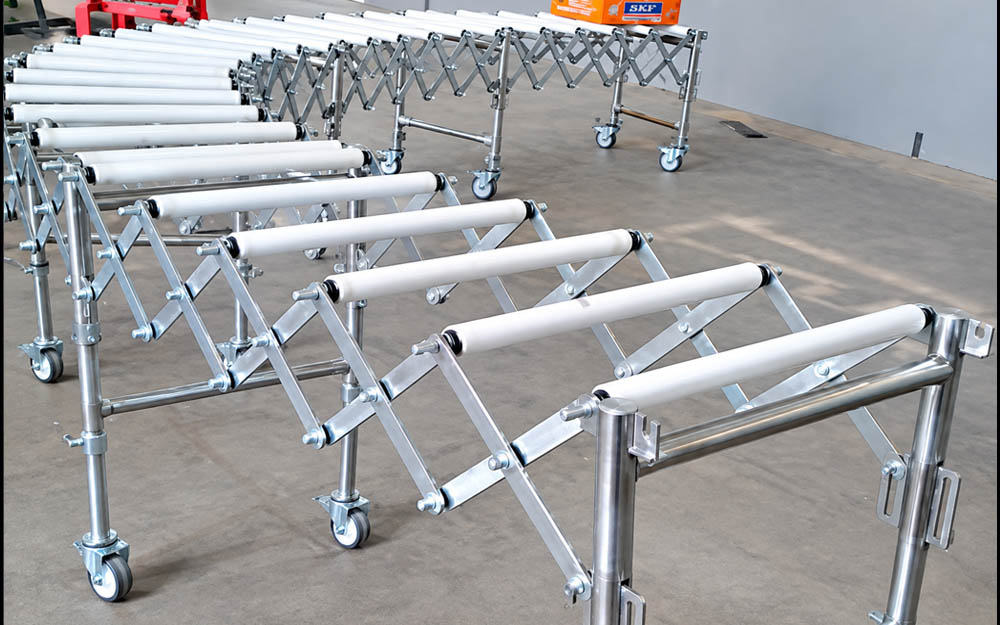
Flexible Conveyors
Flexible expandable conveyors for truck loading and unloading, retail stores, shipping areas, loading docks and plant floors.
Self tracking, height adjustable
06
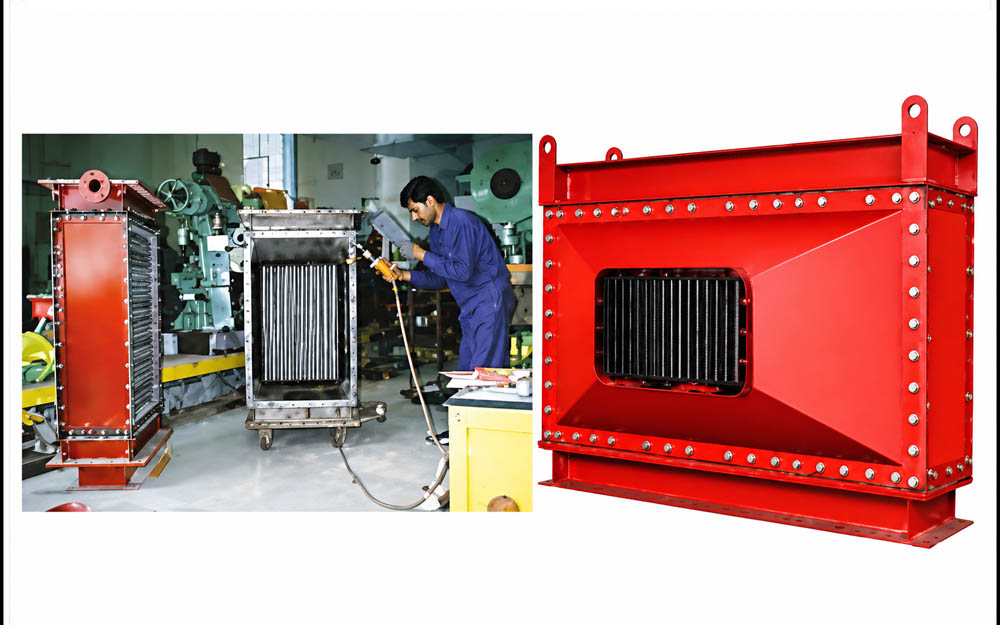
Heat Exchangers
Air-cooled heat exchangers built from quality tubes with spiral-wound SS, MS and copper fins, arranged for maximum face area.
Air cooled, finned tube
Tell us the material and the tonnage
Send the duty, the layout and the plant it is going into. We will come back with the system that suits it.