Typical Rebell solutions
- Bucket elevators
- Screw conveyors
- En-mass conveyors
- Bag stackers
Rebell Engineers supplies material handling equipment and systems on a turnkey basis to the fertiliser sector. Send the material, tonnage and layout, and the system is specified to the duty.
Working in fertiliser?
Tell us the material and the throughput, and we will come back with what suits the plant.
Send requirement
02
Equipment for this sector
01
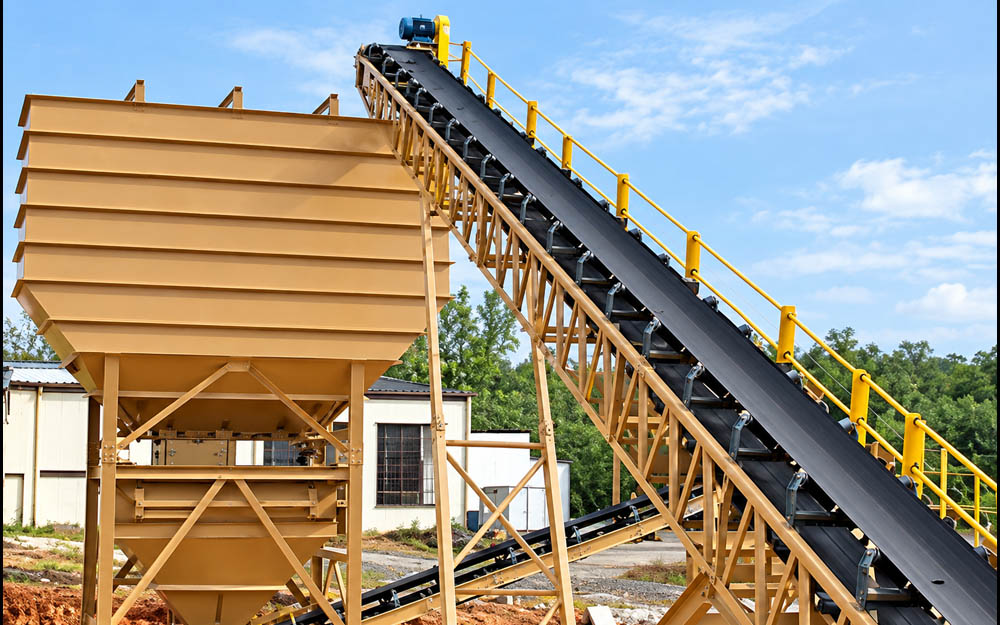
Belt Conveyor Systems
Trough and flat belt conveyors for bagasse, ash, coal, sand, salt and loose sugar, sized to the plant's throughput.
5 – 1000 TPH
02
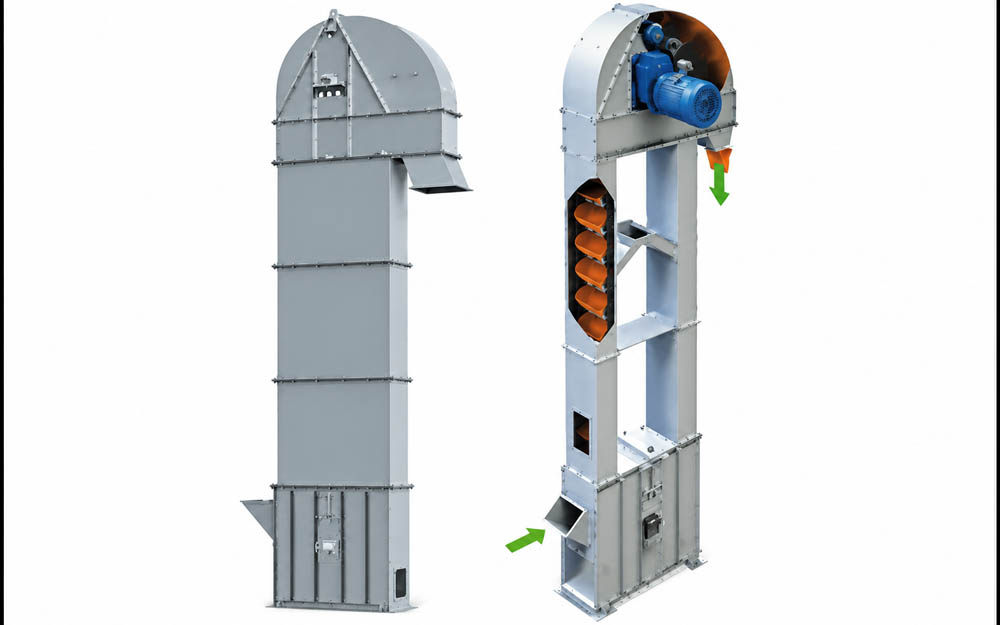
Bucket Elevators
Twin-leg belt type and self-supported chain type elevators for fertiliser, loose sugar, grain, foundry sand, coal and bagasse.
5 – 100 TPH
03
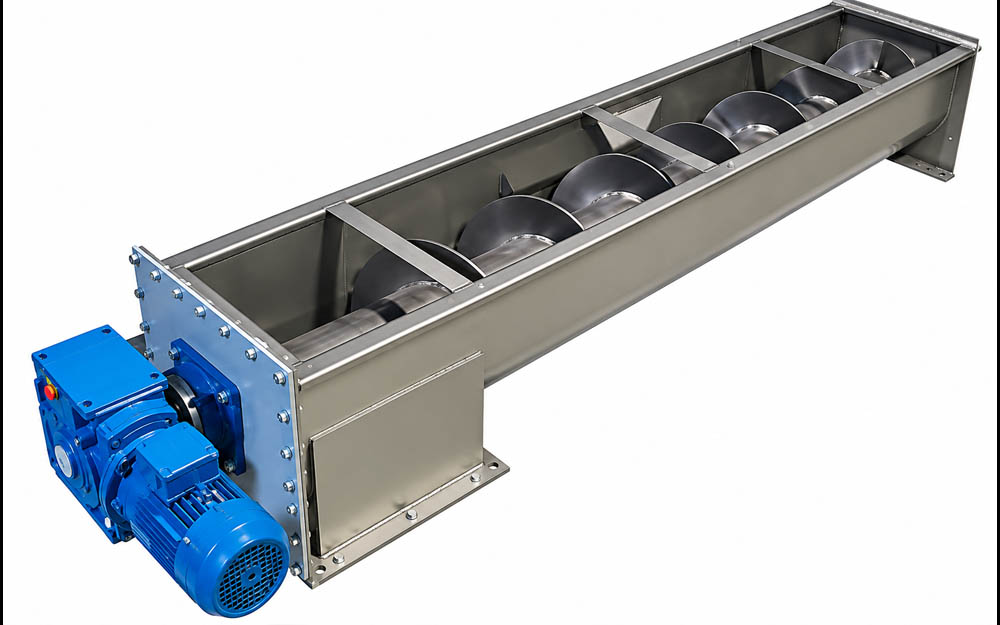
Screw Conveyors
Screw conveyors for sand, grain, sugar, fertiliser, seeds and ash — used across cattle feed, sugar, starch, chemical and fertiliser plants.
5 – 60 TPH
04
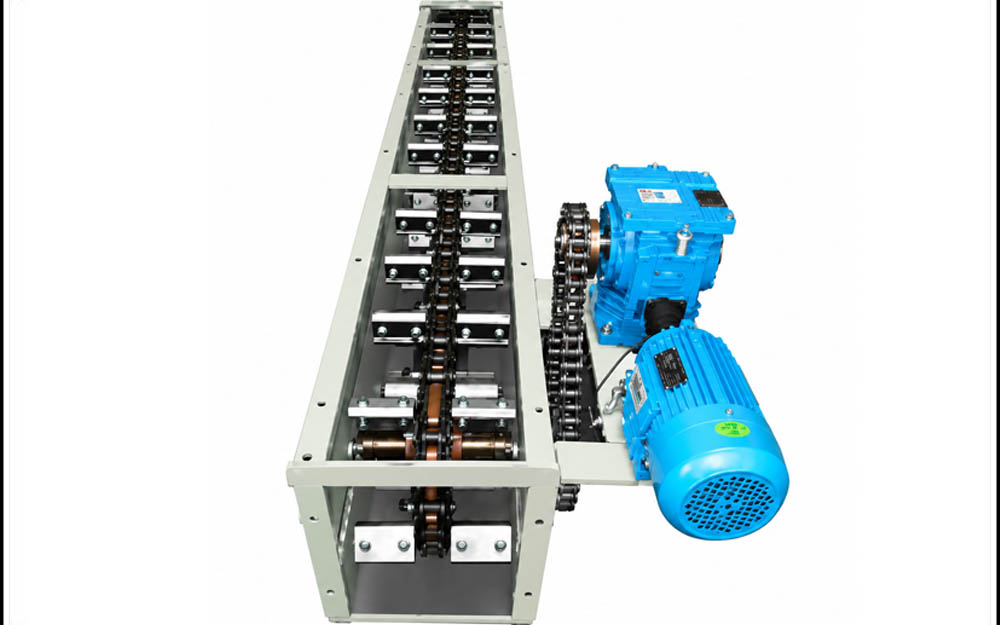
En-Mass Conveyor Systems
Enclosed en-mass conveyors for grain, rice, agro-vet raw material and fertilisers, with dust-free operation.
5 – 150 TPH
05
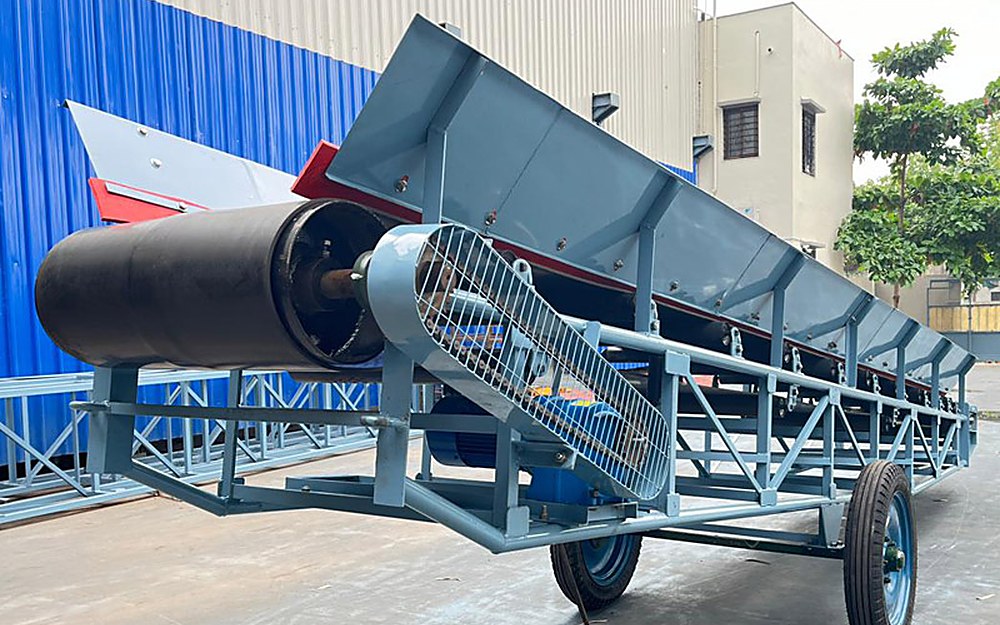
Bag Stackers & Portable Belt Conveyors
Wheel-mounted stackers that cut the manpower needed to stack bags in godowns, with a truck loader variant for loading out.
Mobile, height adjustable
06
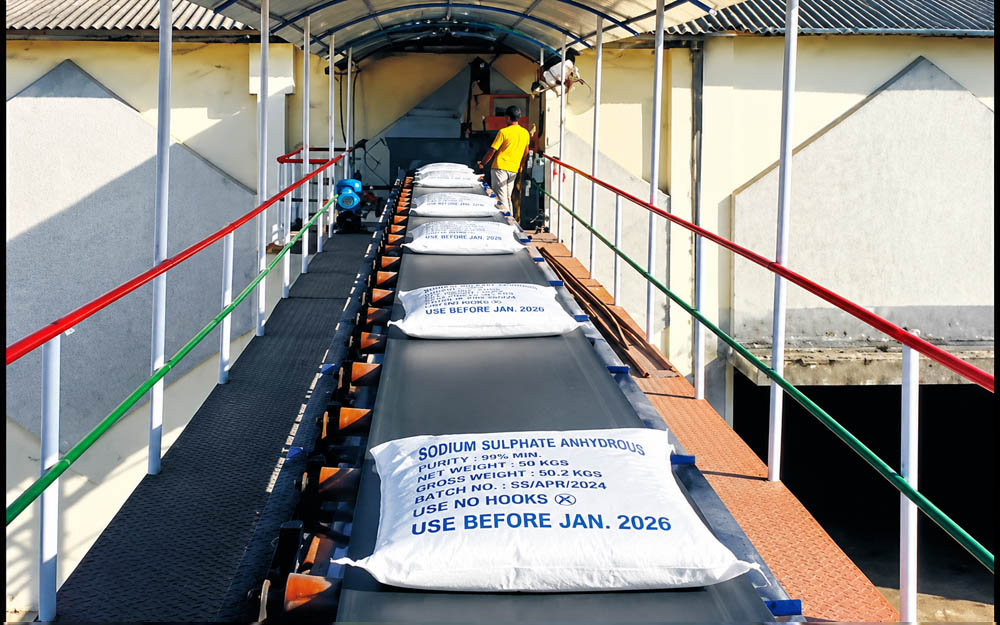
Overhead Bag Handling Systems
Overhead belt and slat conveyor routes that carry stitched bags across a plant without blocking internal transport.
50 – 100 kg bags
Tell us the material and the tonnage
Send the duty, the layout and the plant it is going into. We will come back with the system that suits it.