response@rebellconveyors.com Plot L-42, M.I.D.C. Kupwad, Sangli 416436 +91 92258 18171
Home
Works
Applications
Why Rebell
Quality
Clients
Contact
Request a quote
  1. Home
  2. Catalogue
  3. Bag Handling Systems
  4. Roller Conveyors

Roller Conveyors

Heavy-Duty Roller Conveyors for Smooth and Reliable Material Movement

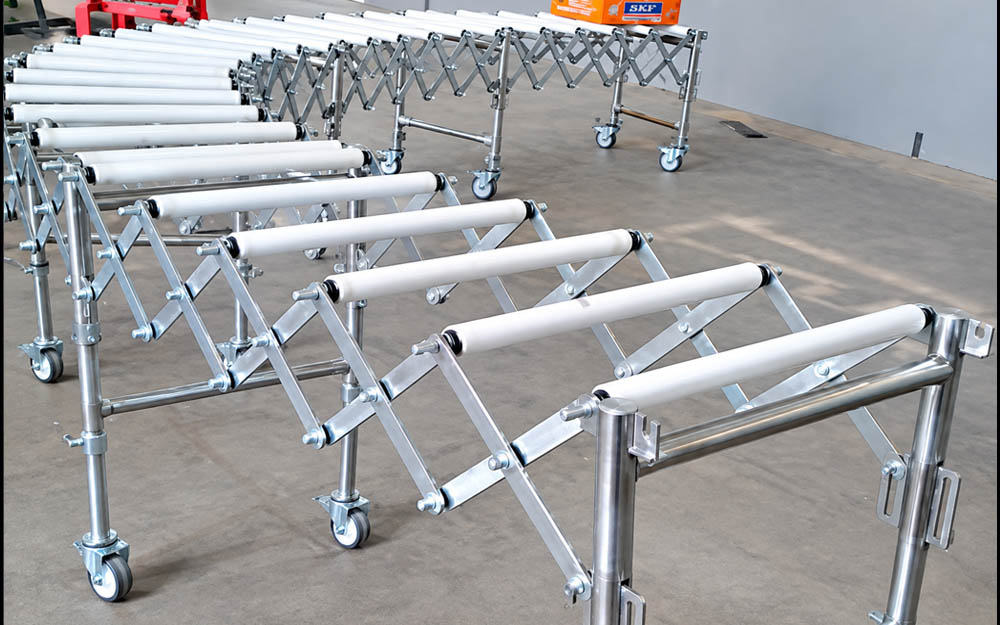
Roller conveyor manufactured by Rebell Engineers Gravity / chain type

REBELL ENGINEERS PVT. LTD. is a leading Manufacturer, Supplier, and Exporter of Roller Conveyors, specializing in both Gravity Type and Chain-Driven Type systems. Our advanced manufacturing setup is located in Sangli, Maharashtra, India, where we design and build reliable conveying systems for industrial applications across multiple sectors.

We manufacture high-performance roller conveyors used for handling castings, cartons, fiber boards, molding boxes, crates, cans, and packaging materials in assembly and packing lines.

Our conveyors are known for their rugged design, efficient performance, and low maintenance, ensuring seamless movement of goods within plants and warehouses.

Roller Conveyors are mechanical handling systems designed to move goods or materials smoothly and efficiently over a series of rollers. They are among the most widely used types of conveyors in industries for transporting boxes, containers, and heavy items without manual lifting.

Key features

  • Heavy-duty design suitable for continuous industrial operation.
  • Smooth, vibration-free conveying with precision-engineered rollers.
  • Available in both powered and non-powered configurations.
  • Adjustable height and modular design for easy installation.
  • Suitable for flat or curved path layouts.
  • Low noise operation with sealed bearing rollers.
  • Custom-built systems to match process and layout requirements.
  • Designed for energy efficiency and operator safety.
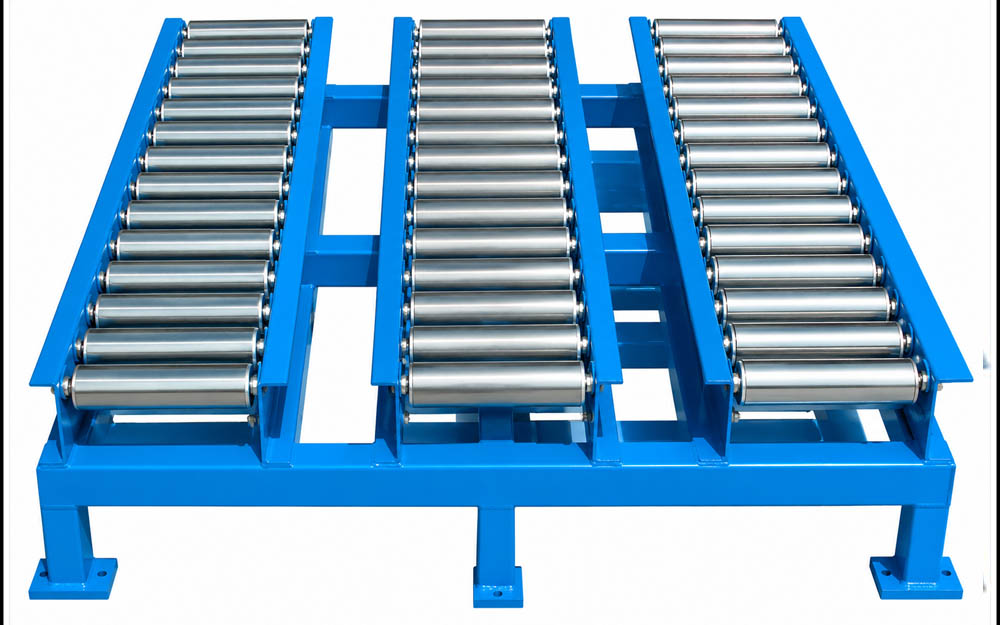
Roller Conveyors

Gravity / chain type

Request a quote
— Technical specifications
Published data. Detailed sizing is confirmed against the duty.
Conveyor TypeGravity / Chain-Driven
Frame MaterialMild Steel (MS) / Stainless Steel (SS)
Roller Diameter38 mm – 114 mm
Roller Pitch75 mm – 150 mm
Conveyor Width300 mm – 1500 mm
Load CapacityUp to 1000 kg/m
Drive TypeChain Drive / Geared Motor
LengthUp to 20 meters (modular)
Surface FinishPowder Coated / Galvanized
OperationManual / Semi-Automatic / Automatic
TypesGravity roller, chain type roller
Loads handledCastings, cartons, fibre board, moulding boxes, crates, cans
01

Gravity Roller Conveyors

Operate on a simple gravity or manual push principle. · Ideal for applications where product movement does not require power. · Used for packing lines, inspection stations, warehouses, and storage zones.

  • Operate on a simple gravity or manual push principle.
  • Ideal for applications where product movement does not require power.
  • Used for packing lines, inspection stations, warehouses, and storage zones.
  • Designed with precision rollers for smooth, noise-free operation.
  • Available in modular sections for easy installation and expansion.
  • Applications: Handling of cartons, crates, cans, fiber boards, and lightweight casting boxes in packaging or inspection lines.
02

Chain-Driven Roller Conveyors

Designed for heavy-duty and continuous operation, powered by chain-driven rollers. · Suitable for moving castings, fiber boards, and heavy crates or boxes in process industries. · Each roller is linked by a precision chain for synchronized movement.

  • Designed for heavy-duty and continuous operation, powered by chain-driven rollers.
  • Suitable for moving castings, fiber boards, and heavy crates or boxes in process industries.
  • Each roller is linked by a precision chain for synchronized movement.
  • Can be integrated with automated packing, loading, or assembly systems.
  • Built to withstand tough industrial environments with minimal maintenance.
  • Applications: Commonly used in foundries, molding lines, component manufacturing, and packaging plants where continuous and controlled conveying is required.

Applications

  • Foundries: Handling of castings, molding boxes, and patterns.
  • Packaging Lines: Smooth transfer of cartons, crates, and cans.
  • Fiber Board & Wood Industry: Conveying of panels and sheets.
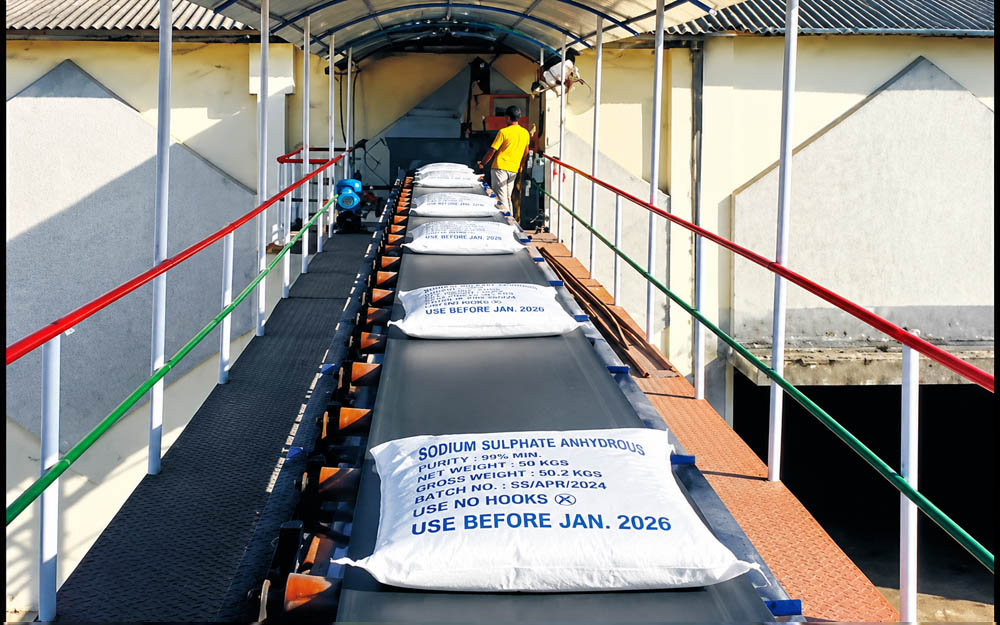
  • Sugar & Fertilizer Plants: Movement of packed bags or boxes.
  • Food & Agro Units: For box and container handling.
  • Warehouses & Distribution Centers: For sorting, inspection, and dispatch lines.
  • Whether for light-duty packaging or heavy casting movement, our roller conveyors deliver dependable performance across all applications.
— In detail

Materials handled

  • REBELL manufactures two main types of roller conveyors:
  • Gravity Roller Conveyors – Operate without power, using gravity or manual push to move loads.
  • Chain-Driven Roller Conveyors – Powered by a chain or motorized drive for continuous movement of heavier loads.
  • Both types are designed for durability, precision, and easy integration with existing production or packaging lines.

Design & Construction

  • Our Roller Conveyors are engineered for strength, stability, and reliability, ensuring long-lasting service even in demanding industrial conditions.
  • Frame: Rigid frame constructed from Mild Steel (MS) or Stainless Steel (SS) for maximum strength.
  • Rollers: Machined rollers with sealed bearings for smooth, friction-free operation.
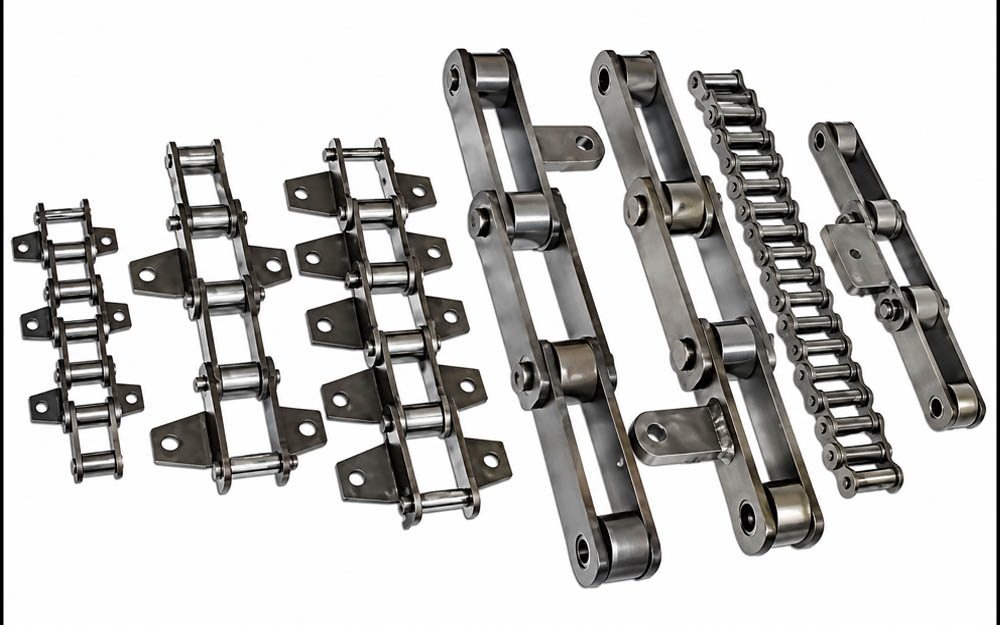
  • Drive Mechanism (for chain type): Chain and sprocket drive connected to a geared motor.
  • Support Stands: Adjustable for different heights and gradients.
  • Surface Finish: Powder-coated or galvanized for corrosion resistance.
  • Side Rails: Provided for safe movement of products and to prevent spillage.
  • Customization: Available in straight, curved, and inclined configurations to suit plant layout.
  • Every REBELL conveyor is designed to deliver consistent performance, low power consumption, and ease of maintenance.

Working Principle

  • The load (casting, carton, or crate) is placed on the conveyor rollers.
  • In a gravity conveyor, the load moves under its own weight or with light manual push.
  • In a chain-driven conveyor, a motorized chain drive rotates the rollers, automatically moving the load forward.
  • The system ensures smooth, uniform movement without product damage.
  • Conveyors can be arranged to move products between processes, packing stations, or storage areas.
  • This makes REBELL's Roller Conveyors a perfect solution for streamlined internal material movement and automated process handling.

Advantages of REBELL Roller Conveyors

  • Proven performance in material handling and packing line operations.
  • High load-carrying capacity with minimal wear and tear.
  • Long-lasting rollers with sealed bearings for dust-free operation.
  • Compact and modular design for easy maintenance and relocation.
  • Customizable configurations to match process flow and space constraints.
  • Smooth integration with other conveyor and automation systems.
  • Backed by REBELL's reliable service and spare parts support.

Integration with Other REBELL Systems

This enables complete automation of material handling — from packing and stitching to stacking, storage, and dispatch. ➡ Visit our Bag Handling Systems page to explore compatible equipment.

  • Bag Stackers / Portable Belt Conveyors
  • Silo Bag Stitching Conveyors / Slat Conveyors
  • Overhead Bag Handling Systems
  • Flexible Conveyors
  • Bag Handling Systems

Quality Assurance

At REBELL ENGINEERS PVT. LTD., we maintain strict quality standards in every stage of design and manufacturing.

  • Dimensional inspection of rollers and frame components.
  • Testing for smooth rolling, noise level, and chain alignment.
  • Load and endurance testing under real working conditions.
  • Anti-corrosion treatment and protective surface coating.
  • Compliance with industrial and ISO standards.
  • Each conveyor system is tested for performance, safety, and reliability before dispatch.

Industries We Serve

✅ Foundries & Casting Units
✅ Sugar & Fertilizer Plants
✅ Food & Agro Processing Units
✅ Cement & Construction Industries
✅ Warehousing & Packaging Centers
✅ Fiber Board & Furniture Units

Why Choose REBELL ENGINEERS PVT. LTD.?

  • Over decades of experience in designing and manufacturing conveyors.
  • In-house design, fabrication, and testing facilities at Sangli, Maharashtra.
  • Customized systems built for each industry's requirements.
  • Proven installations in sugar, fertilizer, packaging, and foundry sectors.
  • Reliable after-sales service and quick spare parts availability.
  • Commitment to engineering precision, quality, and customer satisfaction.

Need this sized for your plant?

Send the material, the tonnage and the centre distance or lift. We will come back with the specification.

Send your requirement