- Home
- Catalogue
- Bag Handling Systems
- Overhead Bag Handling Systems
Overhead Bag Handling Systems
Efficient Overhead Bag Handling Systems for Industrial Applications
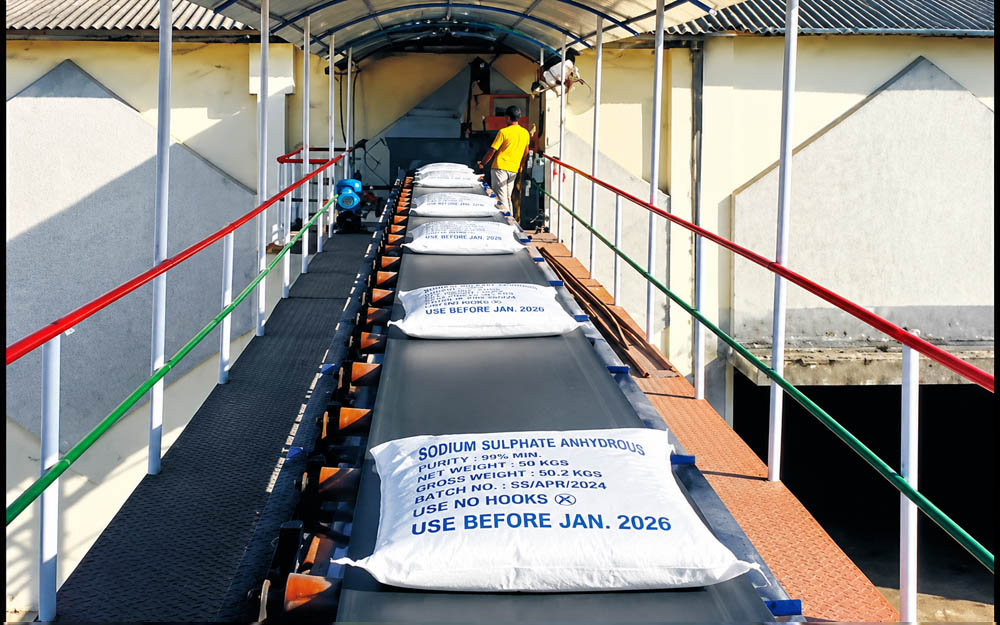 50 – 100 kg bags
At REBELL ENGINEERS PVT. LTD., we specialize in designing and manufacturing Overhead Bag Handling Systems that enable smooth, automated, and space-efficient bag conveying operations.
We are a reputed Manufacturer, Supplier, and Exporter of Overhead Bag Handling Systems, with our advanced setup based in Sangli, Maharashtra, India.
Our systems are widely used in sugar mills, cement industries, fertilizer plants, and co-generation units, where they efficiently transfer stitched bags and bulk materials such as sugar, cement, bagasse, coal, or ash from one section of the plant to another — especially from the production area to the godowns or dispatch section.
An Overhead Bag Handling System is designed to convey filled or stitched bags through an elevated route, keeping the floor area clear for other operations.
These systems generally consist of belt conveyors or slat conveyors installed above ground level to transport bags weighing between 50 kg to 100 kg, typically from the sugar house to godowns or from packing units to storage areas.
In certain industrial applications, such as bulk material handling (bagasse, coal, or ash), overhead conveyor systems are also preferred due to their ability to operate without interfering with internal ground-level transportation or maintenance activities.
Key features
- Overhead installation — keeps floor clear for other processes.
- Suitable for both bagged and bulk material applications.
- Can handle bags weighing up to 100 kg continuously.
- Elevating and lowering arrangements provided for multi-level transfer.
- Custom-designed for any plant layout or building height.
- Robust and low-maintenance construction.
- Energy-efficient operation with smooth conveying.
- Dust-free and safe for industrial environments.
For bulk material applications (like bagasse, coal, or ash), the overhead system carries materials in enclosed conveyors, ensuring dust-free and efficient movement across longer distances.
| Capacity Range | 5 TPH – 200 TPH |
|---|---|
| Conveyor Type | Belt Conveyor / Slat Conveyor |
| Material of Construction | Mild Steel (MS) / Stainless Steel (SS) |
| Bag Weight | 50 kg – 100 kg |
| Bulk Material Handling | Bagasse / Coal / Ash |
| Drive Type | Geared Motor / Chain Drive |
| Elevating & Lowering | Provided as per layout |
| Mounting Type | Overhead / Suspended |
| Operation | Continuous / Semi-Automatic / Fully Automatic |
| Bags handled | Stitched bags of 50 kg to 100 kg |
| Conveyor types | Belt conveyors and slat conveyors |
| Sections | Elevating and lowering overhead systems |
Applications
- Sugar Mills: Conveying stitched sugar bags from sugar house to godowns.
- Cement Plants: Handling heavy cement bags efficiently.
- Fertilizer & Chemical Plants: Transporting filled bags safely over long distances.
- Co-generation Plants: Used for conveying bagasse or ash between processing sections.
- Industrial Warehouses: Automated bag movement between packing and dispatch areas.
- Power Plants: For overhead conveying of coal or fly ash.
Sectors served
Materials handled
- The main advantage of an overhead system is that it maximizes space utilization and ensures uninterrupted workflow within the plant premises.
Purpose & Advantages
The primary purpose of an Overhead Bag Handling System is to automate the transfer of filled or stitched bags from production lines to storage or dispatch points efficiently and safely.
- No Floor Obstruction: The overhead layout ensures the system doesn't disturb any internal movement such as forklifts, vehicles, or workers.
- Continuous Operation: Designed for uninterrupted conveying, ideal for high-output plants.
- Space Optimization: Makes maximum use of vertical space within plant premises.
- Reduced Manpower: Fully mechanized system minimizes manual labor and improves productivity.
- High Reliability: Capable of handling heavy bags or bulk materials continuously.
- Flexibility: Can be customized for both elevating and lowering applications.
Design & Construction
Our Overhead Bag Handling Systems are engineered for durability, performance, and safety. Every system is custom-built to suit the plant layout and operational requirements.
- Construction Type: Available in belt conveyor or slat conveyor configurations.
- Frame & Support: Fabricated from heavy-duty Mild Steel (MS) or Stainless Steel (SS) sections for long life and rigidity.
- Drive System: Geared motor or chain drive arrangement for consistent power transmission.
- Conveyor Path: Designed as an overhead suspended system supported by trusses or beams.
- Elevating & Lowering Sections: Customized lifting and lowering systems for different building levels or process sections.
- Conveyor Belt/Slat: Rubber, PVC, or metal slats selected based on application (bags or bulk material).
- Control System: Optional automated control for speed regulation and start-stop sequencing.
- Safety & Access: Fitted with safety guards, side rails, and easy access panels for inspection and maintenance.
- Every REBELL system is precisely designed for smooth conveying, minimal vibration, and maintenance-free performance.
Sequence of operation
- Feeding: Filled or stitched bags are loaded onto the conveyor from the bag filling or stitching section.
- Elevating: The conveyor elevates the bags along a guided overhead path, clearing all floor-level obstructions.
- Horizontal Transfer: Bags are moved horizontally through the overhead line to reach storage or dispatch areas.
- Lowering / Discharge: At the destination point, the system gently lowers the bags using the lowering conveyor section for stacking or further handling.
Benefits of Using REBELL Overhead Bag Handling Systems
- No Interruption to Ground Traffic: Ensures smooth transportation of materials without affecting internal vehicle or personnel movement.
- Efficient Utilization of Space: Perfect for facilities with limited ground area.
- Reduced Manual Labor: Automation minimizes dependency on manpower.
- High Throughput: Capable of continuous 24x7 operation.
- Flexible Design: Adaptable for various materials and plant configurations.
- Durable and Reliable: Proven systems with long service life.
- Integrated Operation: Can be linked with packing, stitching, and stacking conveyors.
Integration with Bag Handling Systems
- Bag Stackers / Portable Belt Conveyors
- Silo Bag Stitching Conveyors / Slat Conveyors
- Roller Conveyors
- Flexible Conveyors
- This ensures a complete automation cycle — from bag filling and stitching to stacking, transfer, and dispatch.
- ➡ Learn more about our complete range of Bag Handling Systems.
Quality Assurance
At REBELL ENGINEERS PVT. LTD., we follow stringent quality control measures to ensure that each system delivers consistent performance, reliability, and safety.
- Inspection of all components before assembly.
- Load and alignment testing of conveyor systems.
- Drive performance and noise level checks.
- Quality validation for mechanical and electrical systems.
- Final testing under simulated working conditions.
- Every system conforms to industrial and ISO standards, ensuring long-term durability and trouble-free operation.
Industries We Serve
✅ Sugar & Co-generation Plants ✅ Fertilizer & Chemical Industries ✅ Cement & Construction Units ✅ Agro & Food Processing Plants ✅ Power & Biomass Plants ✅ Warehousing & Logistics Centers
Why Choose REBELL ENGINEERS PVT. LTD.?
- Over decades of experience in material handling and conveyor systems.
- Complete in-house design, fabrication, and testing facility.
- Proven track record across multiple industries.
- Custom-engineered solutions for every plant layout and capacity.
- Durable, reliable, and low-maintenance systems.
- Dedicated after-sales and technical service support.
- Commitment to engineering precision and innovation.
Need this sized for your plant?
Send the material, the tonnage and the centre distance or lift. We will come back with the specification.