- Home
- Catalogue
- Bag Handling Systems
- Silo Bag Stitching Conveyors & Slat Conveyors
Silo Bag Stitching Conveyors & Slat Conveyors
Precision Engineered Silo Bag Stitching Conveyors & Slat Conveyors
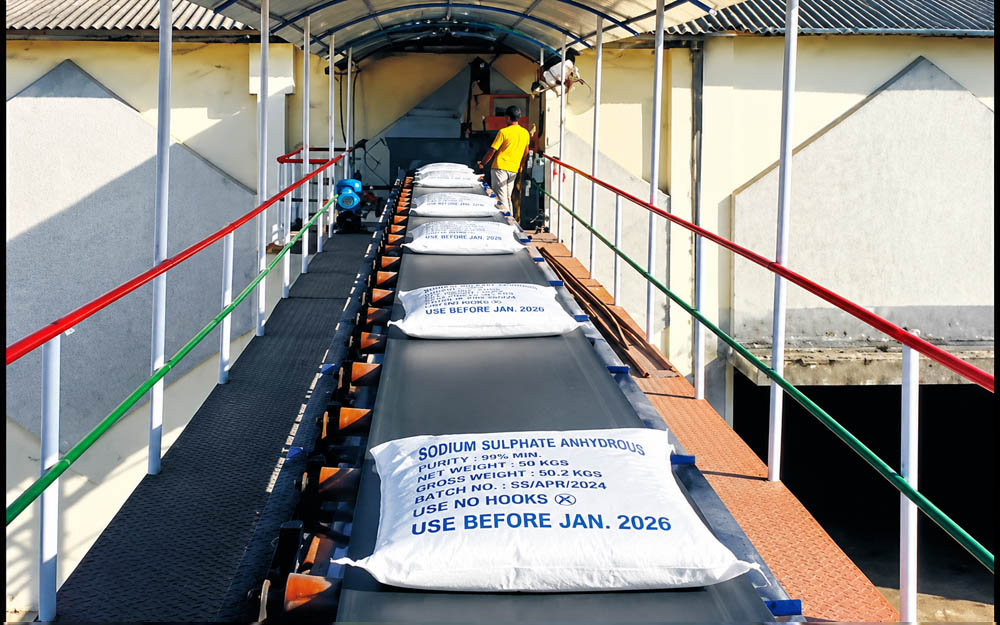 500 – 800 bags/hr
REBELL ENGINEERS PVT. LTD. is a reputed Manufacturer, Supplier, and Exporter of Silo Bag Stitching Conveyors and Slat Conveyors, based in Sangli, Maharashtra, India.
We specialize in providing durable, high-performance conveyor systems for handling stitched bags and industrial materials with smooth, reliable, and continuous operation. Our systems are widely used in sugar mills, cement plants, foundries, and other heavy-duty industrial applications, offering excellent productivity and low maintenance.
Silo Bag Stitching Conveyors are designed for handling stitched or filled bags of products such as sugar, cement, or similar materials. These conveyors are typically installed under silo machines or packing stations to carry filled bags toward stitching or sealing machines and then to the stacking or dispatch section.
REBELL's specially developed Silo Bag Stitching Conveyor System is known for its strength, durability, and precision performance, ensuring smooth operation even under continuous heavy-duty use.
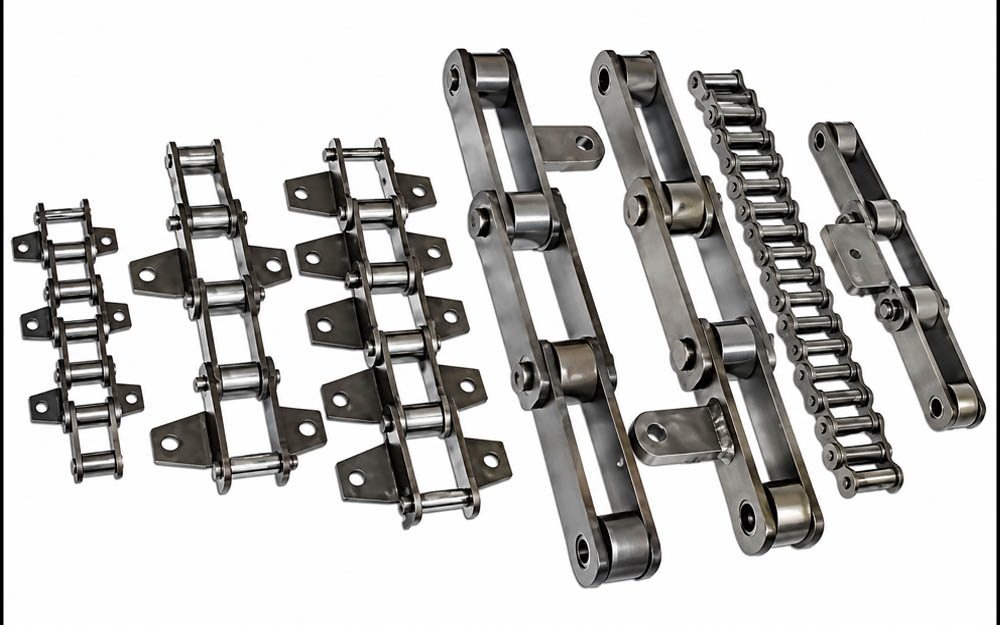
Slat Conveyors are designed for handling scrap, castings, and other heavy-duty materials — commonly used in foundries and manufacturing plants. They consist of a series of metal slats attached to a moving chain, creating a strong and flat conveying surface that can withstand extreme industrial conditions.
REBELL's Slat Conveyors are specially developed for superior performance under continuous operation, with a focus on chain strength, design precision, and reliability.
Key features
- Specially designed for stitched bag handling under silo or packing machines.
- High operational strength for continuous industrial use.
- Heavy-duty construction suitable for 50 kg to 100 kg bag weights.
- Custom-engineered conveyor frame for easy integration with stitching machines.
- Smooth conveying motion ensures precise and clean stitching.
- Operated through a special control panel with paddle-operated switches for easy handling.
- Engineered for low vibration, minimal maintenance, and maximum reliability.
- Durable and corrosion-resistant components ensure long service life.
- Rugged & Reliable: Built for continuous, high-load industrial use.
- Efficient Operation: Smooth conveying motion for precise stitching or heavy material handling.
- Durable Design: Long-lasting chain and slat construction.
- Operator Friendly: Easy control through paddle switch and control panel.
- Low Maintenance: No nylon rollers, minimal wear parts.
- Customizable Layout: Tailored to plant design, space, and process flow.
- Consistent Throughput: Handles up to 800 stitched bags per hour.
| Type | Silo Bag Stitching Conveyor / Slat Conveyor |
|---|---|
| Capacity | 500 – 800 Bags per Hour |
| Material of Construction | MS / SS |
| Chain Pitch | 76.2 mm |
| Chain Link Thickness | 5 mm |
| Operation | Continuous / Semi-Automatic |
| Control | Paddle-Operated Switch Panel |
| Drive Type | Geared Motor / Chain Drive |
| Applications | Bag Stitching, Scrap Handling, Foundry Castings |
| Design | Customizable as per layout |
| Slat design | Without nylon rollers, for heavy working conditions |
Applications
- Sugar Industry: For conveying and stitching sugar bags from silo discharge to stacking zone.
- Cement Industry: For transporting and sealing heavy cement bags.
- Fertilizer Plants: For efficient handling of filled fertilizer bags.
- Agro & Food Processing: For rice, flour, or grain bag stitching and transfer.
- Chemical Industry: For powder or granule packaging lines.
Sectors served
Materials handled
- Capacity: 500 to 800 bags per hour This makes the system ideal for large-scale industrial operations that demand high throughput and consistent reliability.
Design & Construction
- Silo Bag Stitching Conveyors and Slat Conveyors from REBELL are designed using advanced engineering principles and robust construction techniques.
- Heavy-duty structural frame for stability and strength.
- Precision-engineered chain and slat assembly.
- Variable speed geared motor drive for controlled operation.
- Compact, modular, and easy to install under existing silo systems.
- Available in custom lengths, widths, and configurations.
- Built for continuous, vibration-free, and dust-free performance.
Integration with Other Systems
This ensures complete automation from bag filling → stitching → conveying → stacking → truck loading. ➡ Visit our Bag Handling Systems page for complete solutions.
- Bag Stackers / Portable Belt Conveyors
- Overhead Bag Handling Systems
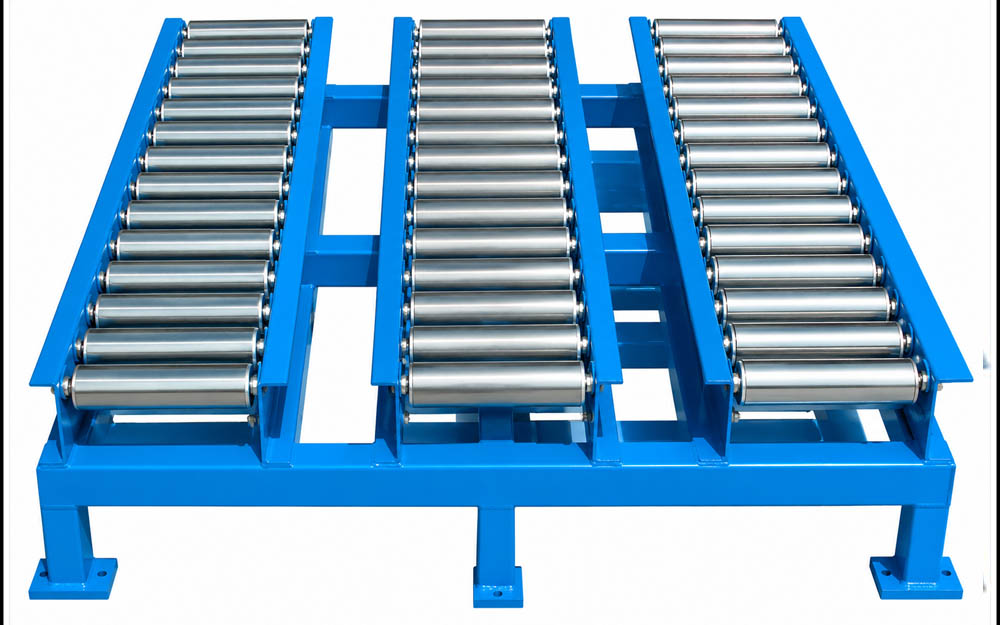
- Roller Conveyors
- Flexible Conveyors
Quality Assurance
At REBELL ENGINEERS PVT. LTD., every system is manufactured with precision and quality control to deliver unmatched performance and reliability.
- Use of tested materials and components.
- Dimensional accuracy and chain tension inspection.
- Load and alignment testing before dispatch.
- Compliance with industrial and ISO quality norms.
- Proven performance in continuous operations across multiple industries.
Industries We Serve
✅ Sugar & Co-generation Plants ✅ Cement & Construction Units ✅ Fertilizer & Chemical Industries ✅ Foundries & Casting Units ✅ Agro & Food Processing Plants ✅ Warehousing & Packaging Facilities
Why Choose REBELL ENGINEERS PVT. LTD.?
- Decades of expertise in industrial material handling systems.
- In-house design, fabrication, and testing facilities.
- Proven performance across India's sugar and cement sectors.
- Custom-engineered solutions for plant-specific layouts.
- Dedicated technical support and after-sales service.
- Focus on durability, innovation, and efficiency.
Need this sized for your plant?
Send the material, the tonnage and the centre distance or lift. We will come back with the specification.