- Home
- Catalogue
- Bulk Material Handling Systems
- Return Bagasse Carriers & Elevators
Return Bagasse Carriers & Elevators
Reliable Return Bagasse Carriers & Elevators for Efficient Bagasse Handling
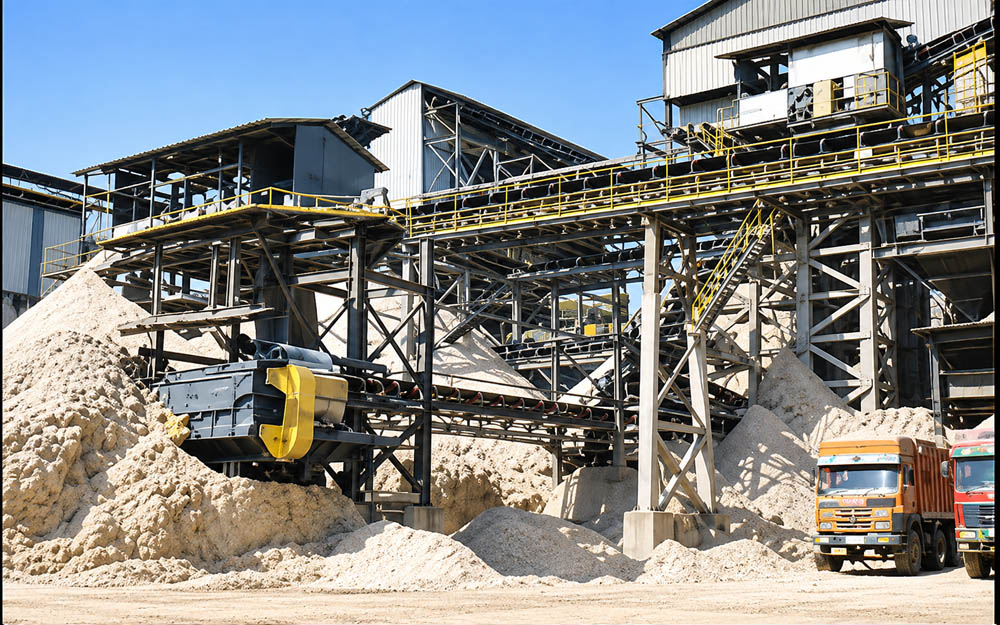 5 – 200 TPH
At REBELL ENGINEERS PVT. LTD., we specialize in designing and manufacturing Return Bagasse Carriers and Bagasse Elevators that offer smooth, efficient, and continuous material handling for sugar industries and co-generation plants.
We are a reputed Manufacturer, Supplier, and Exporter of Return Bagasse Carriers and Elevators, and our advanced manufacturing setup is located in Sangli, Maharashtra, India.
These systems are purpose-built for handling loose bagasse — a by-product of sugarcane crushing — and are widely used for bagasse feeding to boilers, co-generation systems, and other processing units.
Return Bagasse Carriers & Elevators are specialized conveying systems used to transport and elevate bagasse (fibrous residue of sugarcane) from the milling section to the boiler house or storage area.
They are essential components in sugar mills, co-generation plants, and biomass energy units, where efficient bagasse handling ensures continuous boiler feeding and optimized energy utilization.
At REBELL ENGINEERS PVT. LTD., our systems are designed for rugged performance, energy efficiency, and minimal maintenance, ensuring reliable operation even under heavy-duty industrial conditions.
Key features
- Designed for Sugar Industry: Specifically developed for loose bagasse handling and return.
- Continuous & Smooth Operation: Ensures steady bagasse flow with minimal spillage.
- Energy-Efficient: Optimized drive design reduces power consumption.
- Rugged Construction: Built for harsh and dusty industrial environments.
- Customizable Layouts: Designed for both horizontal and inclined conveying.
- Low Maintenance: Simple mechanical design with long-lasting components.
- High Throughput: Handles large volumes efficiently, up to 200 tons per hour.
- Safe Operation: Includes guards and tensioning systems for operator safety.
| Capacity range | We manufacture Return Bagasse Carriers with a capacity range from 5 tons per hour to 200 tons per hour, depending on customer requirements, plant layout, and operational load. |
|---|---|
| Conveyor Type | Horizontal / Inclined / Vertical |
| Material of Construction | Mild Steel (MS) / Stainless Steel (SS) |
| Drive Type | Chain Drive / Geared Motor |
| Speed | Adjustable as per process |
| Application | Bagasse Handling for Boilers and Co-generation |
| Installation | Floor-mounted / Elevated |
| Material handled | Loose bagasse |
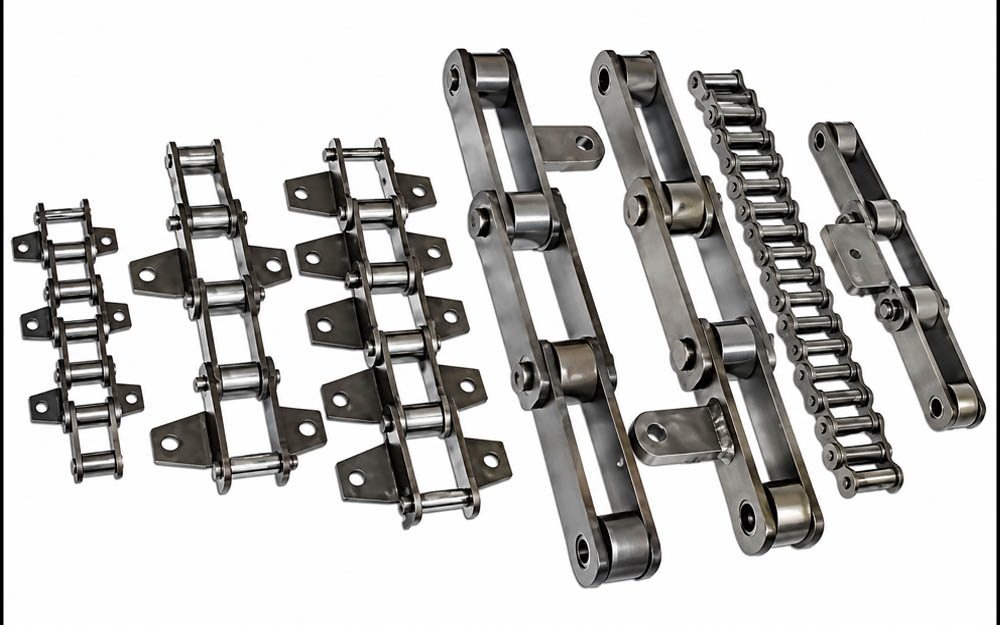
| Chain | RBC chains of 100 mm, 150 mm and 229 mm pitch with swivelling attachments |
Applications
- Sugar Mills – for handling and returning bagasse from the milling section to the boiler.
- Co-generation Plants – for transferring bagasse as fuel for power generation.
- Starch Plants – for handling fibrous by-products.
- Processing Units – where continuous biomass conveying is needed.
- Boiler Feeding Systems – for consistent and automated bagasse feeding.
- Their use ensures streamlined plant operation, optimized fuel utilization, and reduced manual handling.
Sectors served
Design & Construction
All units are designed using modern CAD tools and undergo stringent quality testing to ensure precision alignment, efficient performance, and smooth operation.
- Our Return Bagasse Carriers and Elevators are sturdy, modular, and precision-engineered to handle fibrous bagasse effectively.
- Robust Structure: Heavy-duty steel fabrication ensures long life and durability.
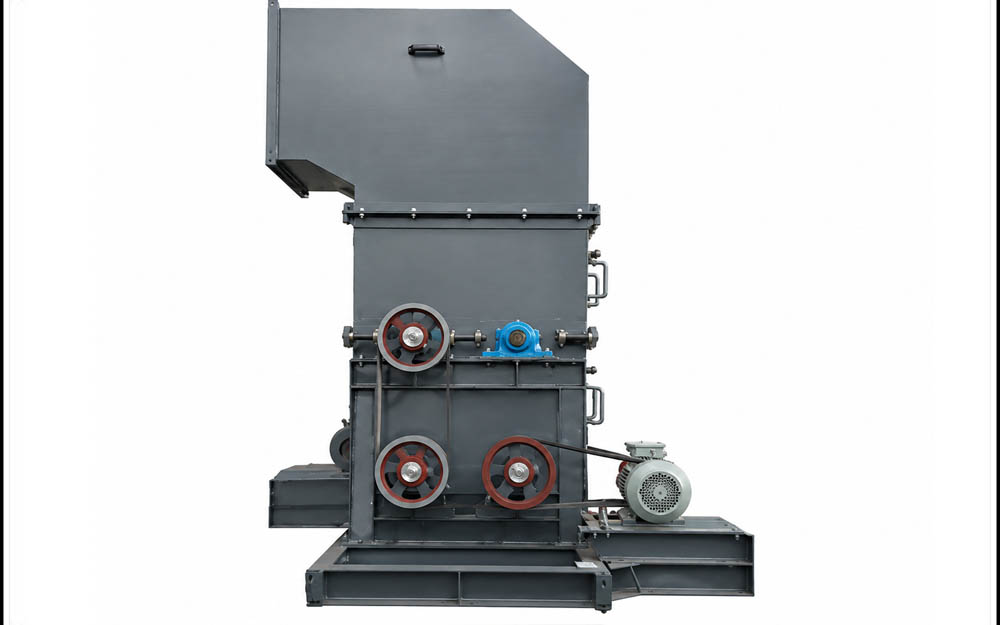
- Drive System: Chain-driven mechanism with adjustable speed controls.
- Trough Design: Open or enclosed type to minimize spillage.
- Inclined / Horizontal Layouts: Custom-built based on mill layout and space availability.
- Safety Features: Fitted with side guards, tension adjusters, and backstop arrangements.
- Ease of Maintenance: Simple access points for inspection and servicing.
- Corrosion-Resistant Finish: For long-term performance in humid sugar mill environments.
How Return Bagasse Carriers & Elevators Work
- Bagasse Collection: Bagasse discharged from the sugar mill is collected in the carrier inlet section.
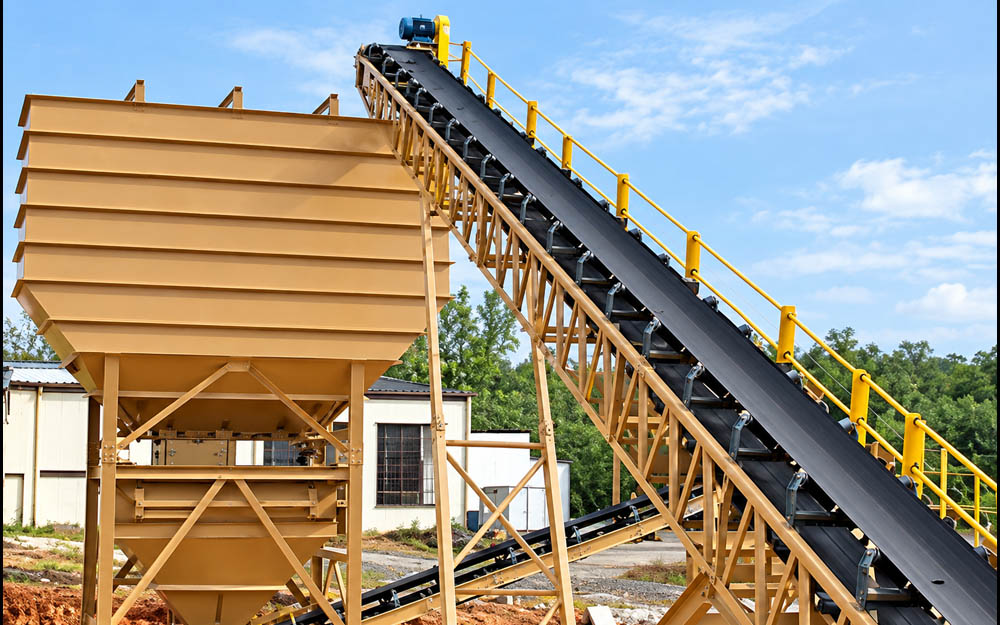
- Horizontal Conveying: The carrier moves the material through a continuous chain-and-slat arrangement.
- Elevation: In the case of an elevator, the system lifts the bagasse vertically or at an incline to reach storage or boiler feeding points.
- Discharge: The material is then fed directly into boilers or transfer hoppers for reuse as fuel.
- This process ensures efficient, automatic, and uninterrupted transfer of bagasse, reducing manual labor and improving overall plant efficiency.
Integration with Other Material Handling Systems
This integrated approach ensures continuous and synchronized material flow throughout the processing plant. ➡ Visit our Bulk Material Handling Systems page to learn more.
- Our Return Bagasse Carriers & Elevators can be seamlessly integrated with other Bulk Material Handling Equipment to create a complete system.
- Belt Conveyor Systems
- Bucket Elevators
- Screw Conveyors
Quality Assurance
Every Return Bagasse Carrier & Elevator manufactured by REBELL ENGINEERS PVT. LTD. is designed and built under strict quality supervision.
- Use of tested and certified raw materials.
- Dimensional accuracy and perfect chain alignment.
- High-quality welding and corrosion protection.
- Operational testing before dispatch.
- Compliance with industrial standards and safety norms.
- Our focus on durability, reliability, and performance ensures that each system offers years of dependable service in demanding plant environments.
Industries We Serve
Our Return Bagasse Carriers & Elevators are trusted across:
✅ Sugar Mills & Refineries
✅ Co-generation Power Plants
✅ Starch Processing Units
✅ Bioenergy & Biomass Power Projects
✅ Boiler Feeding Systems
Why Choose REBELL ENGINEERS PVT. LTD.?
- Expertise You Can Trust: Decades of experience in material handling solutions.
- Proven Track Record: Successful installations across leading sugar and co-gen plants.
- Tailor-Made Solutions: Designed to meet specific process and layout requirements.
- High Efficiency & Low Downtime: Built for reliable, 24x7 operation.
- Comprehensive Support: From design and installation to after-sales service.
- Made in India: Designed and manufactured entirely at our Sangli facility.
Need this sized for your plant?
Send the material, the tonnage and the centre distance or lift. We will come back with the specification.